Prefabrication wins
Where modular packages excel
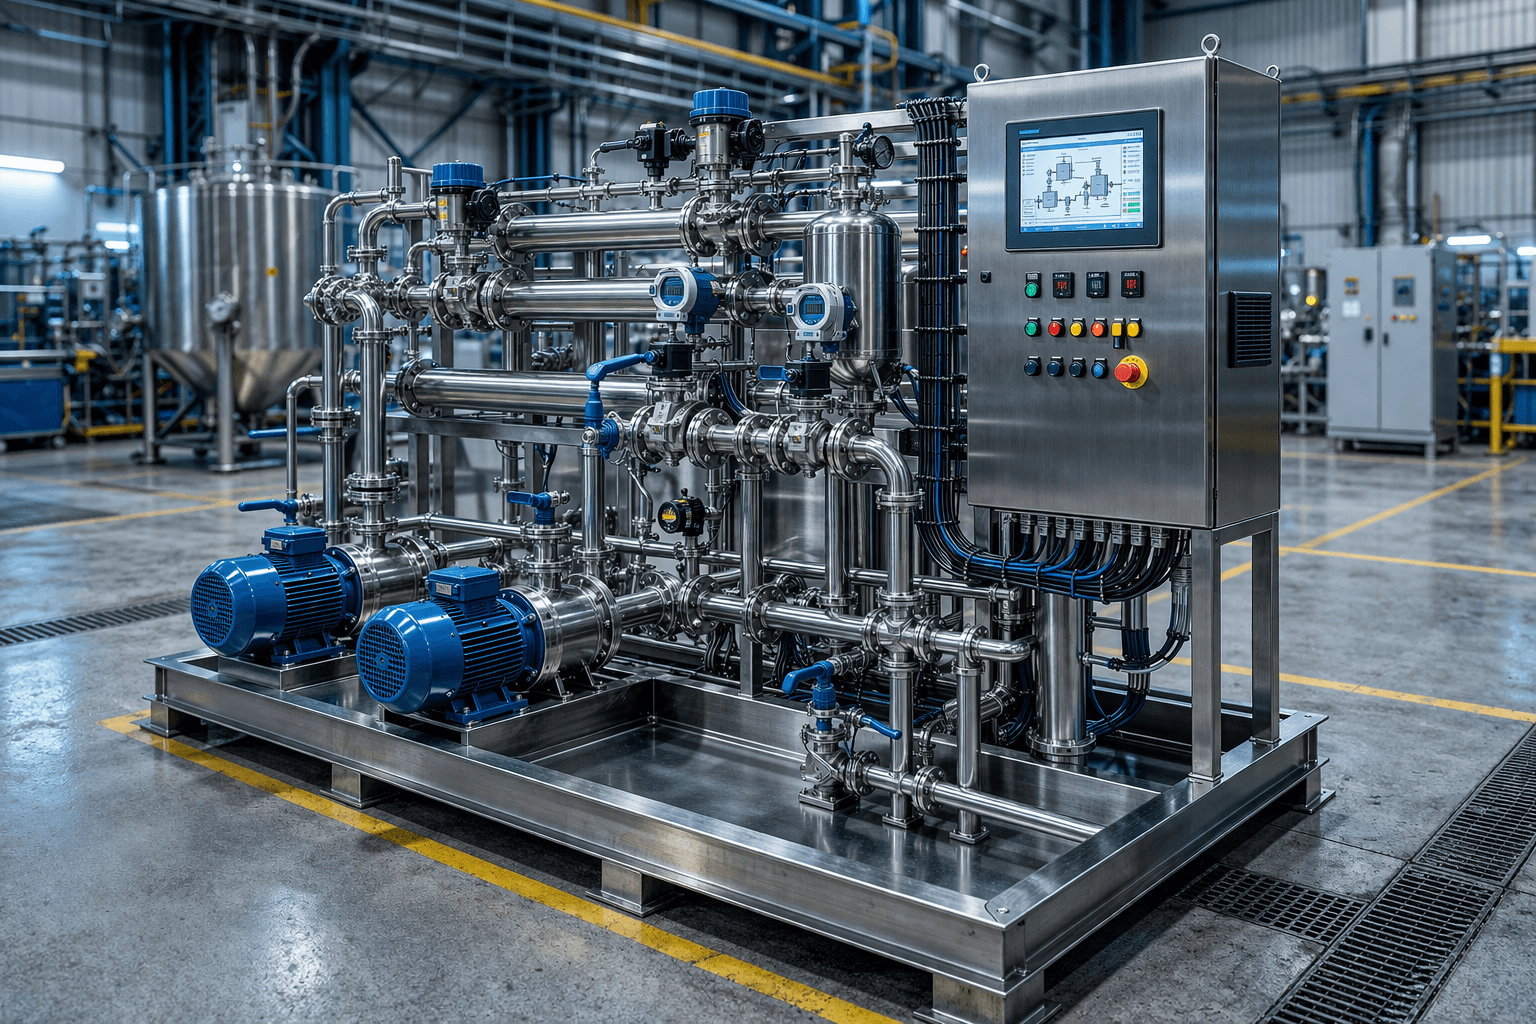
Fabrication under controlled conditions improves weld quality, dimensional control, and FAT before the package reaches a busy plant floor.
For CIP, hot water, transfer, and compact process loops, a skid can compress site duration and reduce hot-work congestion. Civil and utility work can proceed in parallel while the package is built and tested off-site.
Repeatable layouts across multi-line plants reduce engineering rework and spare-parts diversity. Once a proven GA and I/O pattern exists, subsequent lines inherit lessons instead of reinventing routing.
Factory acceptance catches dimensional and functional issues while correction cost is still shop labour. Finding the same issues after setting on foundations is slower and more disruptive.
Documentation tends to be tighter on modular packages because the battery limit is clear. As-built packs, weld maps, and instrument lists travel with a defined system rather than a diffuse field scope.
Modular pays back when schedule criticality and quality control outweigh transport and interface effort.
- Parallel site civil/utility work while the skid is built off-site
- Factory acceptance before shipping
- Repeatable layouts for multi-line plants
- Reduced hot-work and congestion in operating areas
- Clearer documentation boundary at handover
Field routing
When stick-built still wins
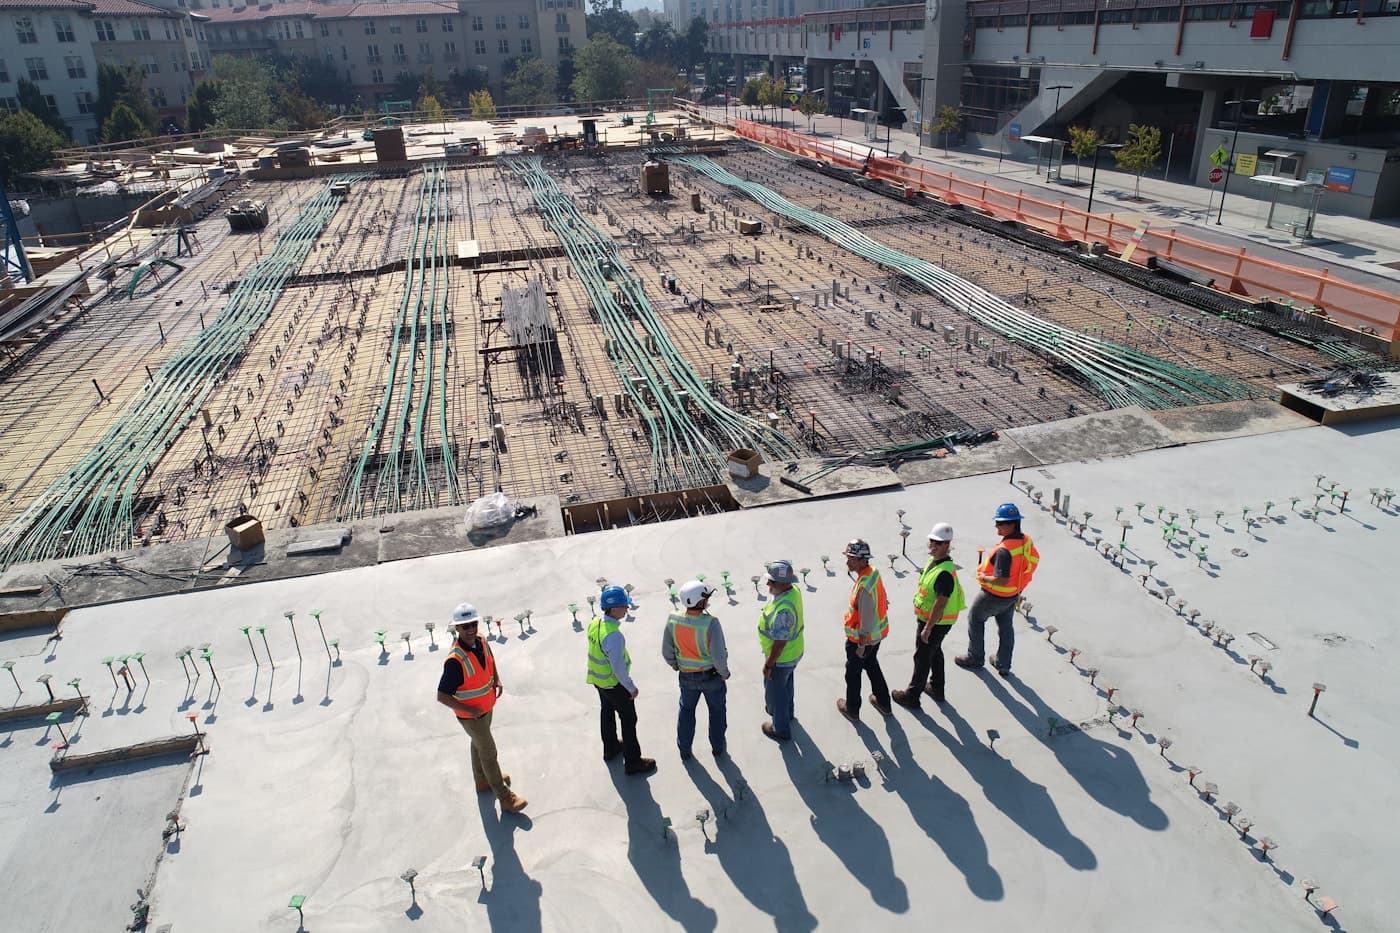
Very large spans, unique site constraints, or one-off tie-ins into dense existing racks may remain more efficient as field piping.
If modular envelopes cannot fit through access routes, doorways, or overhead clearances, the “skid” becomes a field assembly with extra joints and little of the off-site benefit.
One-off connections into congested brownfield racks often need on-site fit-up that defeats prefabrication tolerances. In those cases, shop modules for equipment islands plus stick-built interconnects can be the pragmatic hybrid.
Extremely large diameters or long straight runs may not justify skid framing. The structural overhead can exceed the quality and schedule gain when the duty is simple conveyance.
Local labour availability and permit windows also matter. Where site welding capacity is strong and shop slots are scarce, stick-built can protect the critical path.
Critical path
Schedule and risk comparison
Score the decision on path duration and uncertainty, not only on fabrication unit rates.
Modular shifts labour off the critical site path, but it adds engineering freeze dates, logistics, and interface coordination. Late design changes hurt modular harder because the package is already committed in the shop.
Stick-built absorbs late changes more flexibly, yet it exposes the project to weather, permit sequencing, and competing trades. Quality variation across field crews also widens documentation risk.
Run a simple comparison: weeks of site piping versus weeks of shop build plus transport and set. Include rework probability for hygienic or high-purity duties where field conditions are harder to control.
EPCs should model interface float explicitly. A modular package that arrives early but cannot tie in because utilities are undefined still burns schedule.
If three of four drivers — schedule, access, repeatability, documentation — favour control, modular usually wins.
- Engineering freeze date realism
- Access and transport envelope constraints
- FAT and punch-list closure before ship
- Site trade congestion and hot-work permits
- Brownfield measurement uncertainty
- Documentation and inspection expectations
Assurance
Quality and documentation differences
Shop environments make consistent welding, examination, and dimensional control easier to evidence.
Hygienic and pharma-oriented duties benefit from controlled purge, inspection staging, and cleaner handling of product-contact surfaces. Field conditions can meet the same bar, but they require more temporary controls.
FAT creates a natural documentation checkpoint: tags, certificates, and functional proofs can be closed against a protocol before dispatch. Stick-built often pushes equivalent checks into site commissioning under production pressure.
Turnover packs for modular systems are easier to structure around a battery limit. Field scopes need stronger isometric control to avoid orphan welds and missing certificates.
Neither approach replaces a quality plan. Modular simply concentrates evidence; stick-built distributes it. Choose the model your QA team can actually audit.
Selection method
A practical decision checklist
Use a scored checklist with operations and construction — not a default slogan for either approach.
Score schedule criticality, access, repeatability, and documentation needs on a shared matrix. Weight brownfield measurement risk and utility readiness separately from fabrication cost.
Define hybrid options early: equipment skids with stick-built headers, or stick-built process with modular utility packages. Many plants get the best outcome from selective modularisation.
Confirm transport route, crane capacity, and set-down tolerances before committing. A modular win on paper that fails logistics is a schedule loss in practice.
Document the decision basis so later change requests are judged against the same criteria. That discipline prevents mid-project flip-flops that destroy both shop and site productivity.
- Schedule criticality and float available
- Access, lift, and shipping envelope
- Repeatability across lines or sites
- Inspection and turnover depth required
- Brownfield tie-in complexity
- Change likelihood before engineering freeze
Boundaries
Interface ownership decides success
Modular failures are often interface failures: flanges, utilities, and signals assumed rather than frozen.
Publish a single interface drawing covering mechanical tie-ins, utility conditions, and automation demarcation. Parallel teams invent conflicting truths when that drawing does not exist.
Agree what is tested at FAT versus site. Motors, interlocks, and vendor packages need clear ownership or commissioning becomes a blame loop.
Keep field tie-in isometric responsibility explicit. Dimensional responsibility at the battery limit is where modular and stick-built scopes most often collide.
When in doubt, write exclusions. Ambiguous “by others” language is how tender savings turn into variation orders.
Freeze interfaces early — modular schedule gains disappear when boundaries stay soft.
Takeaway
Klugg engineers both modular and stick-built approaches. We recommend modular when it protects schedule and quality — not as a default slogan. The durable decision is the one your critical path, access constraints, and documentation plan can actually support.
Next step
Need a skid scoped to your URS?
Share process duty, capacity, and standards. We respond with a clear engineering and fabrication path for modular packages.
Keep reading