Design intent
Assembly is not engineering
A skid that “fits the plot” but ignores stress, drainability, or maintainability is expensive to live with.
Long-term reliability is frequently compromised by overlooked fundamentals: nozzle loads, support strategy, cleanability, and how the skid interfaces to utilities and automation. Catalogue selection without a basis of design produces packages that look complete on paper and fail under transport, thermal cycling, or cleaning duty.
Shop convenience often drives instrument placement, valve orientation, and panel location. Operators and maintenance teams then inherit ladders, blocked sight glasses, and devices that cannot be calibrated without removing adjacent equipment.
Engineering depth means freezing duty data, acceptance criteria, and interface ownership before steel is cut. When those decisions are deferred to site, the skid becomes a discovery exercise instead of a controlled deliverable.
Treat every nozzle, drain, and I/O point as a design decision with an owner. If the P&ID, GA, and I/O list disagree, the plant will invent a fourth truth during commissioning.
Is your skid system truly engineered — or just assembled?
Root causes
Where failures usually start
Component catalogues rarely cause the chronic issues; layout density, unsupported spans, dead legs, and unclear I&C ownership do.
Structural frames sized for static weight alone often ignore transport acceleration, lifting points, and pipe stress from thermal growth. Supports that look adequate in the shop can resonate once pumps run against real system head.
Hygienic routing fails when slope, low points, and branch length are secondary to packing density. Residual product or CIP chemistry in pockets creates recurring swab failures that no amount of recipe tuning fully solves.
Automation demarcation is another frequent gap. When the skid vendor and plant I&C team each assume the other owns interlocks, FAT becomes a wiring check instead of a functional proof.
Documentation drift compounds every issue. As-built drawings that do not match nameplates, weld maps, or instrument tags force quality and maintenance teams to reverse-engineer the package under production pressure.
- Structural and pipe stress not checked for transport and operating loads
- Hygienic routing that cannot drain or clean consistently
- Panels and instruments placed for shop convenience, not operator access
- Unclear ownership of valve matrices, interlocks, and I/O lists
- Documentation that does not match the as-built package
- Punch items deferred without owners or site carry-forward
Standards map
How standards reduce risk
EHEDG, 3-A, and ASME BPE do not replace your URS — they give a shared language for cleanability, materials, fabrication, and inspection when your quality plan requires them.
Applying those expectations early — in layout and datasheets — prevents rework after FAT. Clause-level alignment matters more than marketing language such as “BPE-compliant” without a defined scope.
For hygienic duties, cleanability and drainability criteria should appear in the design basis before isometric production. Waiting until fabrication to debate dead-leg length or surface finish guarantees change orders.
Material and weld strategies should be traceable to the duty: product contact, utility contact, and non-contact zones need different control levels. Mixing those zones without a matrix creates audit friction later.
Standards are most useful when they are mapped to inspection and turnover evidence. A clause without a corresponding record in the pack is a claim, not a control.
Map standards to clauses and evidence early — not as a late stamp on the cover sheet.
Mechanical integrity
Stress, supports, and transport reality
If the package cannot survive lifting, road transport, and thermal growth, operating reliability never gets a fair chance.
Define lifting and shipping load cases in the structural calculation, not as an afterthought for the rigger. Soft points under pumps, exchangers, and stacked vessels are common sources of permanent misalignment.
Pipe stress should consider nozzle allowables, guide and anchor strategy, and how field tie-ins will load the skid boundary. Over-constrained field connections often show up as flange leaks months after start-up.
Access platforms, drip trays, and cable tray routes affect stiffness and maintainability together. Cutting them to save envelope usually transfers cost to scaffolding and downtime later.
Agree shipping orientation, centre of gravity, and tie-down points before packing. Damage that looks cosmetic at arrival can shift instrument calibration and seal faces enough to fail first-pass commissioning.
- Transport and lift cases in the structural basis
- Nozzle load checks against vendor allowables
- Anchor/guide plan for thermal growth
- Protected instrument and panel locations for shipping
- Clear CG and lift-point documentation for logistics
Buyer checklist
What to demand from a skid partner
Ask for a clear basis of design, approval drawings, FAT evidence, and a turnover pack your quality and maintenance teams can use without reverse-engineering the skid.
A usable engineering pack ties P&ID, GA, nozzle schedule, and utility list into one coherent story. If those documents disagree, stop fabrication until they align.
Material and weld strategy should be written, not implied. Product-contact finishes, examination methods, and certificate depth should match the URS and site quality plan.
FAT is only as strong as the protocol. Dimensional, pressure, functional, and documentation hold points need acceptance criteria before the witness day.
Turnover should leave the plant with as-built drawings, certificates, and a punch register with owners — not a folder of generic vendor PDFs.
If the pack cannot support an audit or a maintenance intervention, the skid is unfinished.
- P&ID-aligned layout and nozzle schedule
- Material and weld strategy documented
- FAT procedure and records with clear criteria
- As-built drawings and certificates
- Interface drawing for utilities and automation
- Open-item register carried into site commissioning
Design gates
Catch issues before steel is cut
Formal design reviews with operations, quality, and I&C catch the failures that drawings alone hide.
Hold a layout review focused on drain paths, maintenance envelopes, and operator sight lines — not only equipment fit. Walk the 3D model as if you are starting up and cleaning the line.
Freeze interface conditions early: flange ratings, utility setpoints, signal types, and battery limits. Late interface changes are among the highest-cost revisions on modular packages.
Use a risk register for hygienic and mechanical hotspots. Dead legs, unsupported spans, and ambiguous interlocks should be closed before release to fabrication.
When schedule pressure tempts teams to “fix it on site,” document the residual risk explicitly. Deferred design is still design debt — it only changes who pays interest.
Takeaway
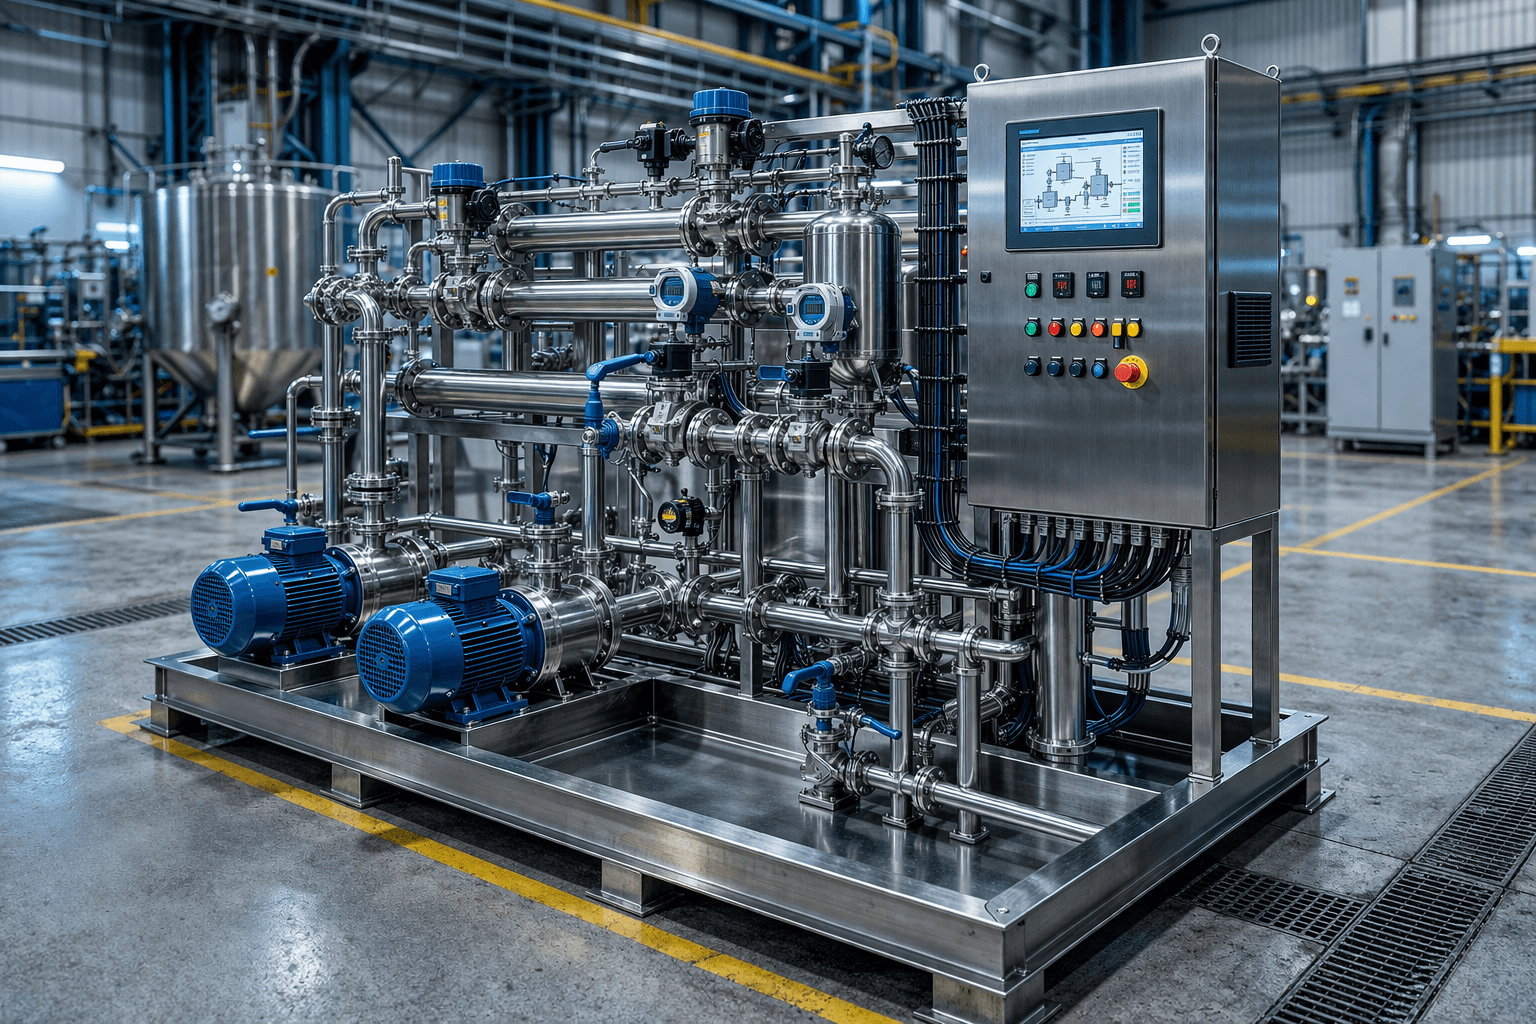
A process skid is an integrated engineering system. Cutting design depth may reduce upfront cost, but it raises operational risk across cleaning, maintenance, and automation. Reliability starts on the drawing — not only on the shop floor — and standards earn their value when they are applied early with evidence.
Next step
Need a skid scoped to your URS?
Share process duty, capacity, and standards. We respond with a clear engineering and fabrication path for modular packages.
Keep reading