Single source
Freeze the interface drawing
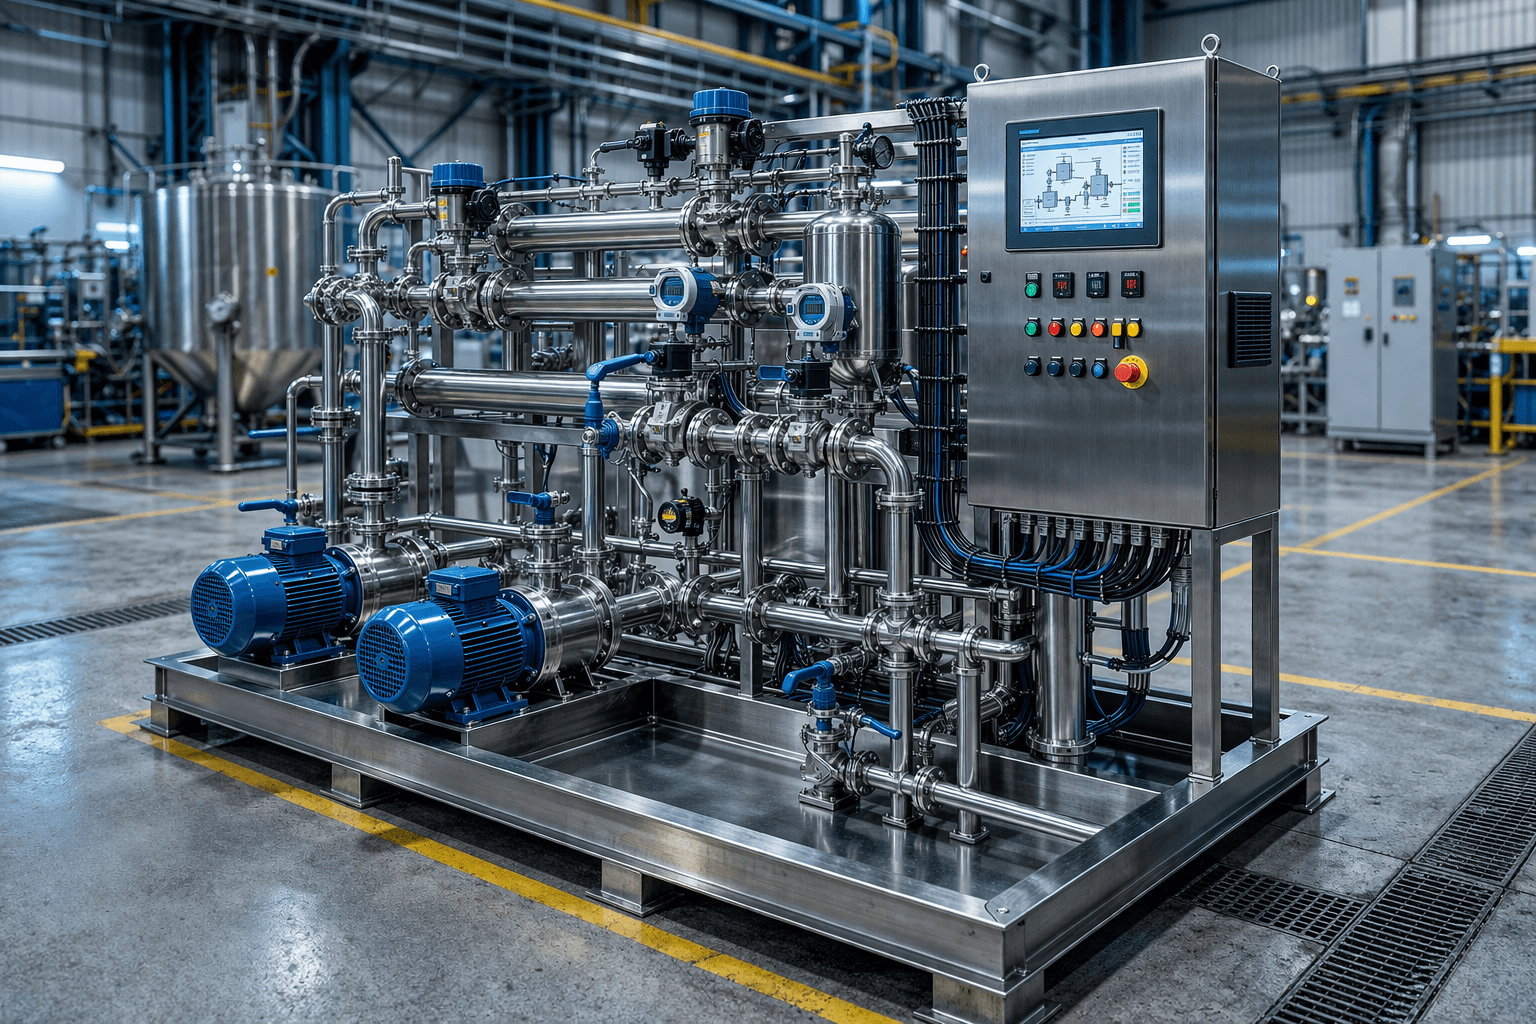
A single interface drawing — mechanical tie-ins, utility conditions, and signal list — prevents parallel teams from inventing conflicting truths.
Publish battery limits for piping, power, pneumatics, drains, and data. Soft boundaries encourage each contractor to draw the line where it is commercially convenient.
Revision control matters. Interface drawings that lag the P&ID create silent mismatches in flange ratings, setpoints, and tag names.
Include physical access notes for mating flanges and cable entries. A correct flange that cannot be reached with a torque wrench is still a failed interface.
Require formal acknowledgement from process, piping, electrical, and automation leads before fabrication release. Silent dissent surfaces later as RFIs.
If the interface is not on one controlled drawing, it is not frozen.
Utility data
Mechanical and utility conditions
Assumed pressures, temperatures, and qualities are among the most expensive errors on modular utility packages.
State supply and return conditions with units, ranges, and design versus normal values. “Plant steam available” is not a datasheet.
Define fluid quality expectations where relevant: clean steam, WFI-adjacent utilities, compressed air dryness, or cooling water fouling factors. Wrong assumptions drive wrong materials and instruments.
Clarify drain and vent destinations, including hazardous or sterile segregation rules. Field teams should not invent discharge paths in classified spaces.
Agree which side owns flexible connectors, spectacle blinds, and first isolation valves. Those small items generate outsized variation orders.
- Pressure/temperature envelopes at each tie-in
- Utility quality and cleanliness assumptions
- Drain/vent routing ownership
- Flange standards and gasket specs
- First isolation and temporary strainer scope
I&C package
What automation teams need from the skid vendor
Clear instrument list, signal types, fail-safe behaviour, and demarcation of what is tested at FAT versus site.
Align the I/O list to the site tag philosophy before panel design. Renaming after wiring wastes both shop and site labour.
Document signal types, ranges, and power sources for each device. Ambiguous “4–20 mA” without loop power ownership still causes brownfield conflicts.
State fail positions and interlock summaries where in scope. Automation engineers need cause-and-effect intent, not only a wiring table.
Define which sequences are vendor-skidded versus site-DCS owned. Split-brain control is a common source of incomplete FAT and unsafe workarounds.
Hand the I&C team a coherent package — not a box of instruments and a verbal briefing.
- I/O list aligned to tag philosophy
- Panel boundaries documented
- Cause & effect or interlock summary where in scope
- FAT versus site test split for loops
- Network/protocol demarcation if applicable
Compliance pack
GMP-oriented documentation at the boundary
Interface clarity should appear in the turnover pack the same way materials and welds do.
Include as-built interface drawings, instrument datasheets, and calibration certificates tied to tags. Qualification teams sample boundaries as often as they sample welds.
Record any site-dependent tests deferred from FAT with rationale. Hidden deferrals resurface as protocol deviations.
Keep change control on interface revisions after approval. Untracked “small” flange or signal changes break alignment with validated assumptions.
Map URS interface requirements to deliverables so auditors can follow the chain without project archaeology.
Prove-out
FAT scenarios that prove the interface
Test the boundary conditions you claim — not only the devices in isolation.
Simulate utility availability faults and confirm alarms and fail-safes respond as documented. Happy-path demos hide the behaviours that stop batches.
Verify connector pinouts, terminal numbering, and cable schedules against the interface drawing during FAT. Paper alignment is not enough.
Where media cannot be supplied in the shop, use agreed simulations and list residual site tests explicitly. Do not imply full proof you did not perform.
Invite the site automation lead to witness boundary tests. Early disagreement is cheaper than PLC rewrite after installation.
- Fault and fail-safe scenario list
- Terminal and cable schedule checks
- Documented residual site tests
- Witness attendance from plant I&C
- Punch ownership for interface gaps
Lessons
Common interface failure patterns
Most painful delays repeat the same avoidable mismatches.
Flange rating or facing mismatches at the battery limit remain common when vendors and EPCs use different default standards. Freeze the standard in the URS and interface drawing.
I/O count creep without panel space or PLC card planning creates late electrical redesign. Freeze signal lists with contingency rules.
Utility quality surprises — wet air, dirty cooling water, unstable steam — damage instruments and control valves after start-up. Challenge assumptions with site data early.
Unclear drain ownership in classified areas leads to noncompliant field fixes. Design the compliant path before the skid ships.
Interface risk is project risk — price and schedule it explicitly in the modular plan.
Takeaway
We build utility and process packages with explicit automation interfaces so your I&C team is not reverse-engineering the skid on site. Predictable pharma utility skids share one frozen boundary drawing, proven FAT scenarios, and a documentation pack that matches tags to signals. That discipline turns modular delivery into schedule protection instead of integration debt.
Next step
Need a skid scoped to your URS?
Share process duty, capacity, and standards. We respond with a clear engineering and fabrication path for modular packages.
Keep reading